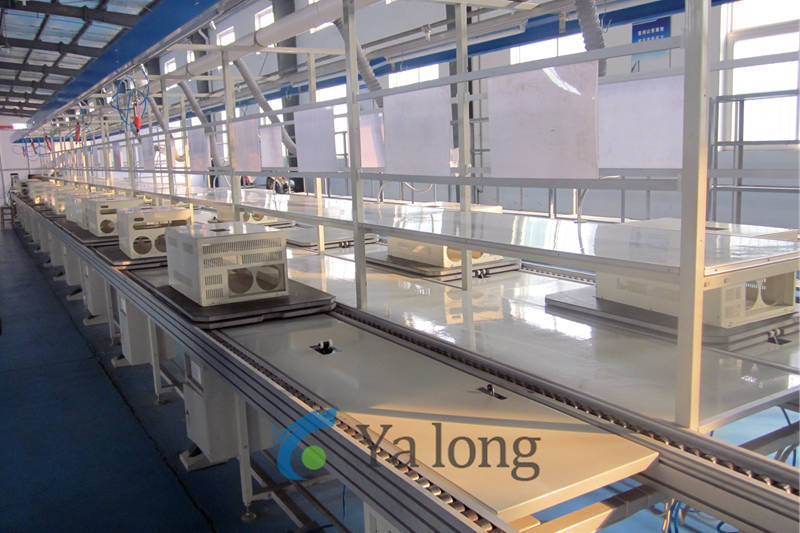
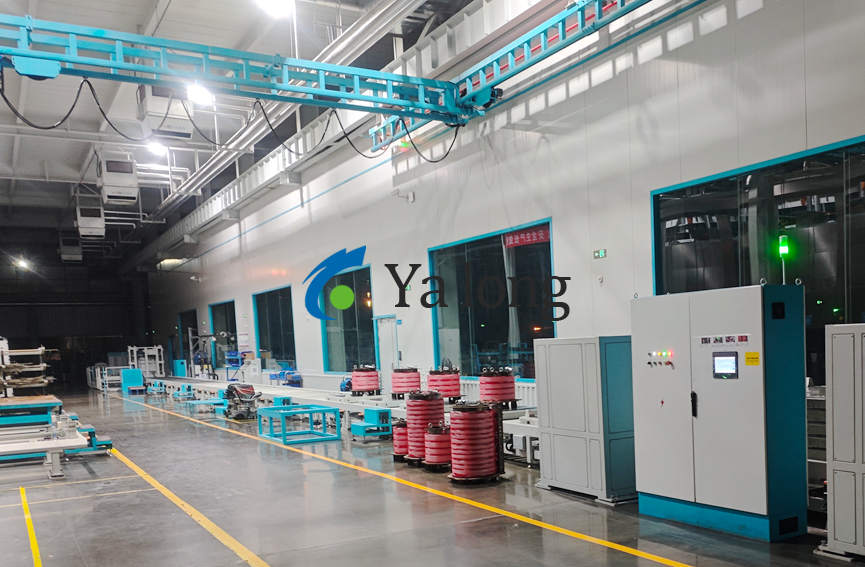
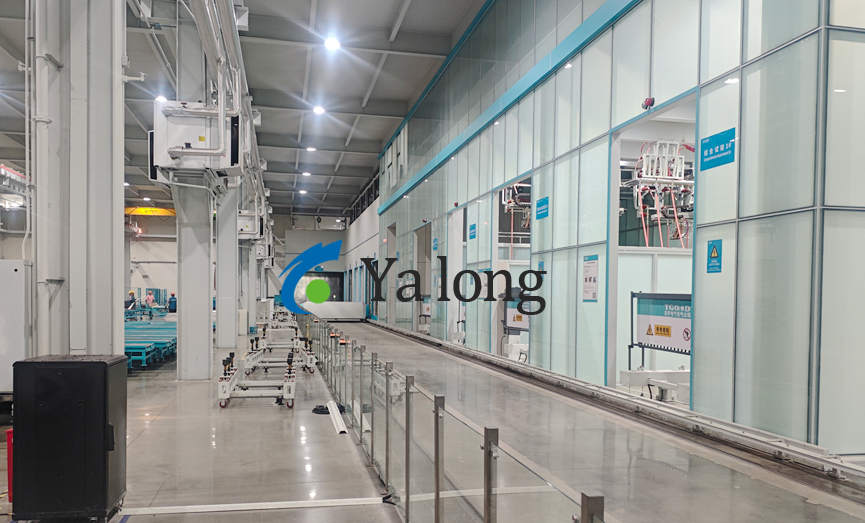
I. This transformer assembly line covers the entire process from coil molding, vacuum resin casting, and high-temperature curing to final assembly material handling. It is organized according to a three-tier architecture: “Equipment Automation + Logistics Automation + Information Integration.” The production line is custom-designed (non-standard) based on the customer’s facility conditions, product portfolio, and capacity targets. It is suitable for high-volume production of 10kV distribution transformers as well as multi-variant manufacturing of 35kV/110kV special transformers.
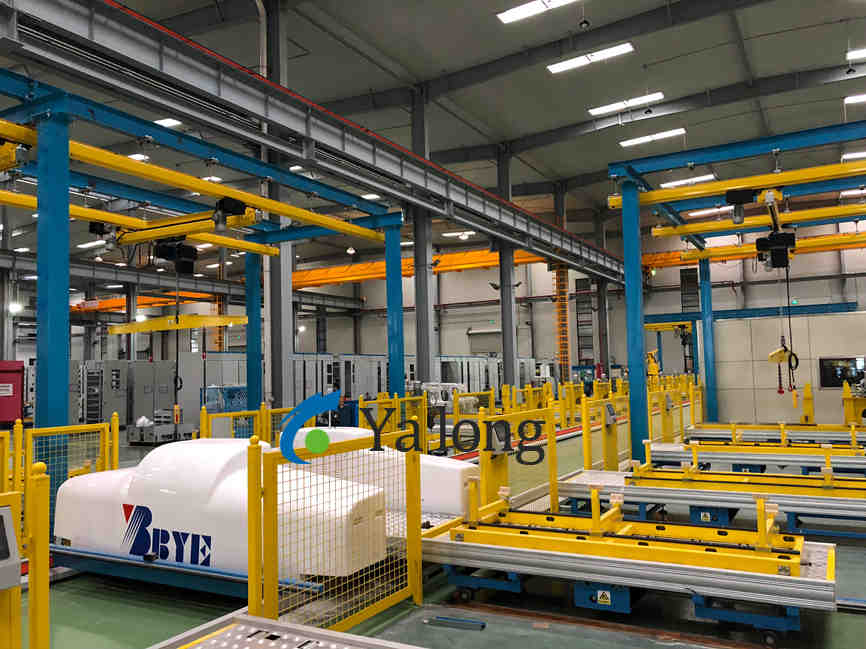
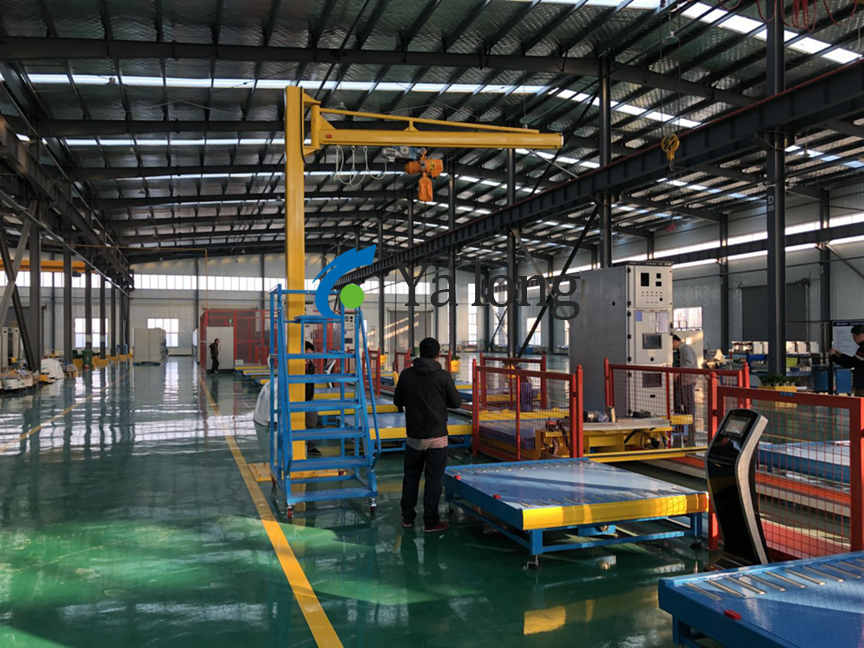
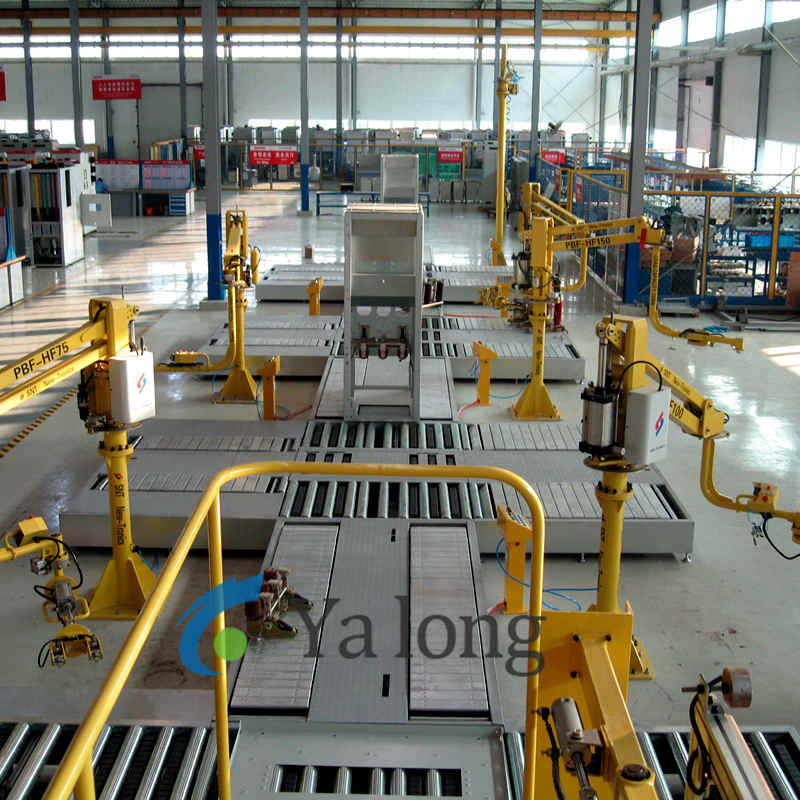
II. Front End — Mold Loading & Material Preparation Area: KBK flexible overhead crane systems are deployed to cover coil storage, mold loading stations, mold preparation areas, and RGV transfer points. After coils are loaded into molds, they are placed on tooling racks, awaiting retrieval by the logistics system.
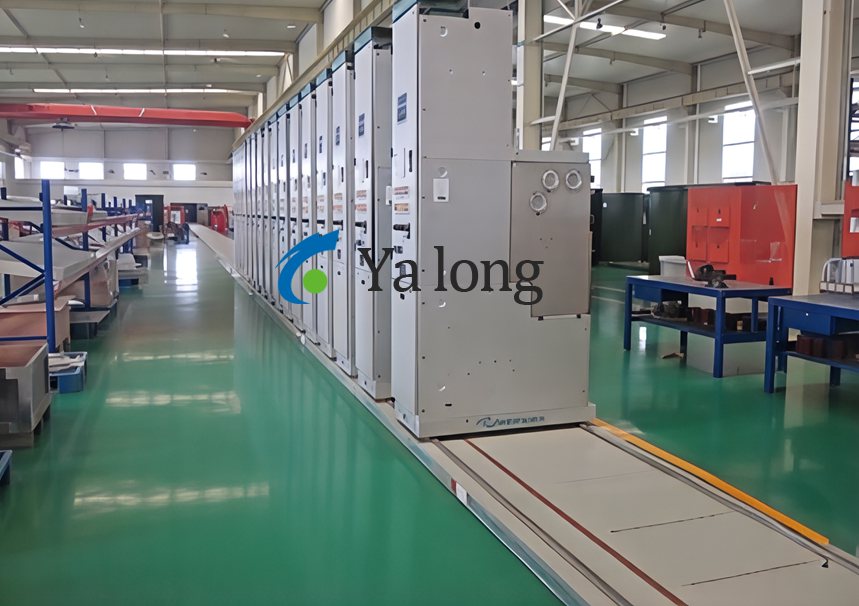
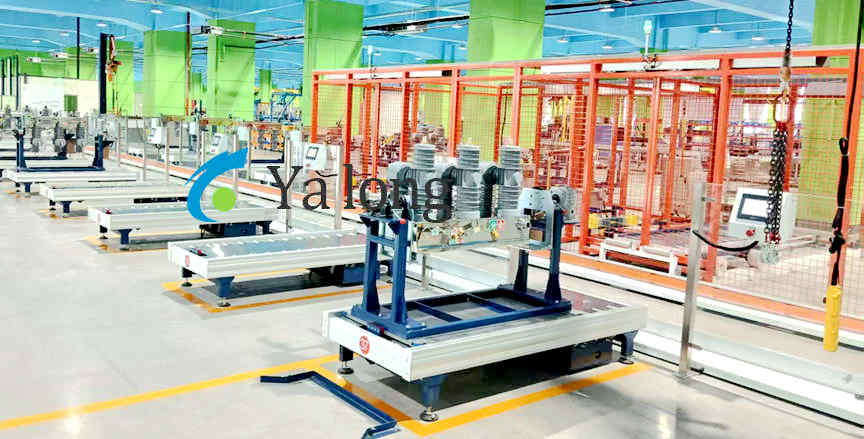
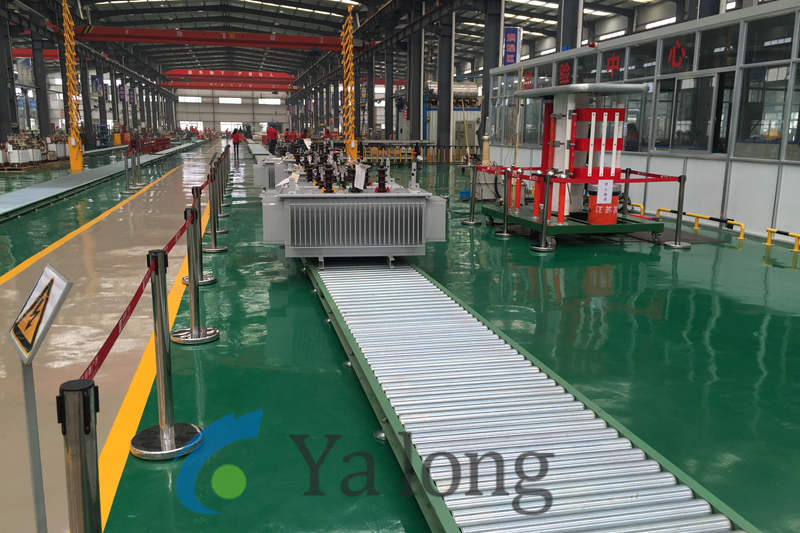
Middle Section — Vacuum Casting & Curing Area: Casting tanks and curing ovens are arranged in rows. RGVs (Rail Guided Vehicles) circulate along floor-embedded tracks between equipment, delivering tooling racks to casting stations, curing oven inlets, and outlet buffer zones.
Back End — Demolding & Post-Processing Area: After curing, molds are returned by RGVs. KBK cranes assist with mold opening, part removal, and mold cleaning. Finished coils then proceed to final assembly or testing processes.
All zones are coordinated via a master PLC interfacing with the MES (Manufacturing Execution System), ensuring synchronization among material supply, process execution, and output takt time.
III. Key Equipment & Process Capabilities
- Vacuum Pressure Casting System
Resin and hardener are stored separately in preparation tanks, degassed via thin-film deaeration, and then metered into a final mixing tank by precision pumps in precise ratios. The mixture is injected into the mold cavity under vacuum; positive pressure can be applied during the process to enhance impregnation. The system allows for adjustable operating vacuum levels, casting temperatures, and pressures, controlling dosing accuracy and mixing uniformity. The entire casting process is automatically controlled by a PLC, with operators selecting corresponding process recipes for execution. - High-Temperature Curing System
Curing ovens utilize electric heating combined with hot air circulation. Multi-segment PLC temperature control supports preheating, gelation, curing, and slow cooling curves. Multi-point temperature acquisition ensures uniform temperature distribution within the oven, minimizing risks of resin cracking and shrinkage. Multiple curing ovens can operate different curing curves simultaneously. - Logistics & Crane Systems
KBK aluminum alloy track networks cover mold loading and transfer areas, featuring low deadweight and minimal running resistance. RGV rail cars rely on physical guide rails for operation, offering high positioning accuracy unaffected by floor conditions, making them ideal for cyclic delivery of heavy-duty tooling racks. RGVs and KBK systems collaborate to form a closed-loop logistics system.
IV. Technical Specifications (Customizable)
| Parameter Item | Reference Range | Customization Notes |
|---|---|---|
| Plant-Wide Logistics System | ||
| RGV Rated Load | 1t / 2t / 3t / 5t / 10t | Customized based on max. tooling rack weight |
| RGV Track Length | 10m – 100m+ | Customized based on workshop length |
| RGV Positioning Accuracy | ±1mm / ±2mm | Customized based on docking equipment precision |
| RGV Communication | Industrial Ethernet / Wi-Fi / 5G | Customized based on site network conditions |
| KBK Track Coverage Area | 50㎡ – 500㎡+ | Customized based on facility area |
| Vacuum Casting Equipment | ||
| Vacuum Level Range | 10Pa – 1000Pa (Adjustable) | Customized per process requirements |
| Resin Metering Accuracy | ±0.5% – ±2% | Customized per accuracy requirements |
| Casting Tank Inner Diameter | Based on max. mold size | Non-standard design |
| Simultaneous Mold Capacity | 1–4 molds/tank | Customized based on capacity needs |
| Curing Oven Cluster | ||
| Single Oven Power | 15kW – 60kW | Customized based on chamber volume |
| Temp. Control Segments | 4–16 segments | Customized based on process complexity |
| Door Opening Mechanism | Vertical Lift / Horizontal Slide | Customized based on shop layout |
| Simultaneous Operating Ovens | 2–10 units | Customized based on capacity needs |
| Information System | ||
| Communication Protocols | PROFINET / Modbus / OPC UA | Customized based on client systems |
| Data Acquisition Points | 50–500 points | Customized based on requirements |
| MES Integration | Supported / Optional | Customized based on IT planning |
| Facility Requirements | ||
| Floor Load Bearing | ≥ 2t/㎡ – 5t/㎡ | Customized based on equipment layout |
| Overhead Crane Interface | Optional | Customized based on existing cranes |
| Power Supply | AC 380V 3-Phase 5-Wire | Customized based on total power load |
Note: All parameters above are reference values. All items can be custom-designed according to specific customer requirements.
V. Non-Standard Customizable Configurations
- Space Customization: Design of KBK track spans, RGV dimensions, track routing, and equipment arrangement based on facility column spacing, ceiling height, and crane interfaces.
- Product Customization: Customization of fixtures, mold specifications, casting tank volumes, curing oven temperature profiles, and process recipes based on the product spectrum.
- Capacity Customization: Matching takt time through parallel oven positions, dual RGV configurations, and buffer zone capacities.
- Automation Level Customization: Supports various automation levels from manual-assisted to fully automatic; phased implementation available.
- Informatization Customization: Pre-integrated MES/ERP interfaces; configurable data acquisition scope, report types, and traceability depth as needed.
VI. Digitalization & Information Integration
By connecting KBK cranes, RGV logistics vehicles, vacuum casting equipment, and curing oven clusters via Industrial Ethernet into a unified control network, the system enables:
- Production order dispatching and scheduling
- Remote calling and locking of process recipes
- Equipment status monitoring and fault alarming
- Tooling flow path planning and tracking
- Automatic quality data collection and report generation
VII. Application Scenarios
This production line integrates casting, curing, and assembly into a continuous manufacturing system, reducing inter-process waiting and handling while supporting continuous production. Rail-based logistics and zoned protection achieve human-machine separation. It is applicable to new factory construction and automation retrofits of traditional workshops for dry-type transformer manufacturers, serving transformer production needs in sectors such as renewable energy substations, rail transit power supply, and data center power distribution.